What Makes Fibre Laser the Superior Choice for Cutting Reflective Metal Sheet?
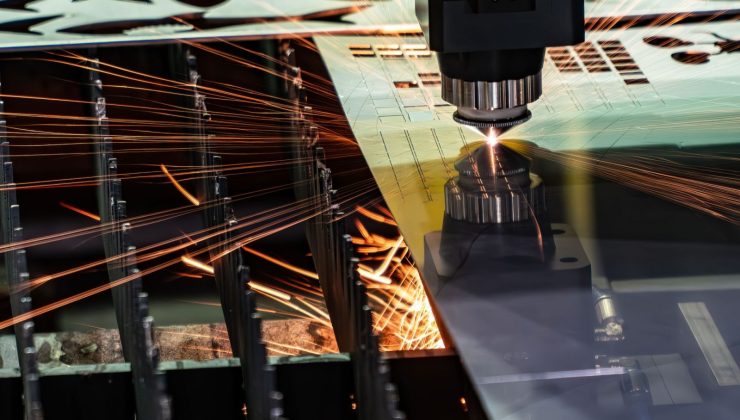
| Quick answer: Fibre lasers have a short 1-micron wavelength. Metals that reflect lots of light cantakein this light well. This lets the laser cut fast, cleanly, and safely. It also keeps the laser’s parts safe. |
Cutting non-iron materials that reflect light, like aluminum, copper, brass, and silver, has always been hard for people who work in making things. Gas-based lasers, which are common, often have a hard time with these. The bright surfaces act like mirrors, so the laser energy bounces away instead of going into it.
Today, people use new machines in this work to get jobs done quicker. With expert laser cutting aluminium services, companies get good results and feel sure there is less risk of mistakes. This process helps companies meet their goals for making parts. There are no issues like sharp edges or heat hurting non-ferrous alloys.
Fibre laser uses a new way to work on this old problem. It changes how light works with pieces of metal.
Understanding the Physics of Metal Reflectivity
Metals absorb light at different speeds. The speed changes based on the beam’s wavelength that lands on their surface. Older laser machines give out light at longer wavelengths. This is around 10.6 microns. At this level, bright aluminum, copper, and brass can send back up to 95% of the beam’s energy.
Fibre lasers use a shorter wavelength, which is about 1.08 microns. At this point, the energy gets into many non-ferrous metals faster.
- Better Ability to Soak in Energy: More of the energy be in the beam. It goes through shiny stock fast.
- Higher Power Density: A fibre laser send all its power to a small spot. This makes the top melt quickly, before it can bounce the light back.
- Stable Processing: When energy goes in without stopping, you get clean and even cut lines. This works well, even if thickness changes.
Elimination of Back-Reflection Risks
Back-reflection happens when light hits the surface of the stuff and goes back to the laser source the same way. In older laser systems, back-reflection can cause big problems. It can burn mirrors, break important parts, and damage the whole system. Fixing this can cost a lot.
Fibre lasers keep their parts safe inside by using strong design ideas.
- Solid-State Beam Transport: Light goes through soft glass fibers instead of bare mirrors in the air. This keeps the power safe inside a closed setup.
- Optical Isolators: Hardware sensors find the light that comes back. They turn its way or stop it from reaching the laser seeds.
- Adaptive Beam Change: Special optics fix the shape of the beam when in use so that it fits the surface.
Operational Advantages Across Industry Applications
Switching to fibre lasers when you work with shiny materials has clear benefits. You get faster speed. You will also pay less to run it. The look of the surface will be better too.
| Feature | Fibre Laser Systems | Traditional CO2 Lasers |
| Energy Absorption Rate | Extremely High (1.08 µm wavelength) | Low (10.6 µm wavelength) |
| Cutting Speed (Thin Sheets) | Up to 3x Faster | Baseline Standard |
| Optics Maintenance | Minimal (No alignment mirrors) | High (Requires frequent mirror cleaning) |
| Operational Power Usage | Lower overall power consumption | Higher energy demand |
| Back-Reflection Safety | Built-in fiber optics protection | High risk of optical module damage |
Speed and Throughput Efficiency
Fibre lasers send heat into the material much quicker. This means you can cut thin to medium shiny sheets at a much faster speed. When you cut faster, there is less heat that can change how your work looks. This helps the work keep its correct size and shape.
Precision Edge Finish
When you use more energy, the width of the cut gets smaller. This can help reduce the slag and dross that forms under the parts you cut. A cleaner cut means you do not have to spend much time on extra work like removing burrs or finishing by hand.
Broad Material Compatibility
Fibre laser systems can work with tough industrial things with no trouble.
- Aluminum Alloys: Easy to use and does not leave heat marks on the surface.
- Yellow Brass & Copper: Cuts fast and does not stop working because of reflected light.
- Stainless & Galvanized Steel: Cuts clean at the edge. When you use nitrogen gas, there is less oxidation.
Cost-Effectiveness and Long-Term Value
Adding fiber equipment to the shop can help save money. This works for both small custom places and large factories. Solid-state fiber systems do not use moving mirrors inside. They also do not have laser gases that need to be changed. This helps lower the cost of upkeep.
When you work with special alloys, you can use expert laser cutting aluminium services for your projects. This way, you get help from cost-saving fiber systems. You do not need to spend much money on buying big machines yourself.
Frequently Asked Questions
Why do reflective metals damage older laser systems?
Reflective metals can send the longer light waves back into the cutting head. This beam goes up the optical path. It can make the parts hot and may cause breaks inside the mirrors, lenses, and beam delivery parts.
Can fibre lasers cut copper and brass safely?
Yes. A fibre laser has a short wavelength. Copper or brass can take in this light very fast. A solid-state optical system helps stop any energy that bounces back from hurting the laser source.
What assist gas works best for cutting reflective metals with a fibre laser?
Nitrogen works best as an assist gas when you need to cut shiny metals like aluminum and stainless steel. It cools the part where you cut and keeps it from rusting. This helps make the edge very bright. You get a good edge for welding too.
Fibre lasers are still the main tool people use for cutting and making things like shiny sheet. They use a wavelength that is easy to absorb. The laser beam is sent through a solid path. This lets fibre systems stop the old problem where light bounces back. These lasers work fast. They cut things well, even when dealing with tough mixes.